Fewer variants. Less complexity. Greater efficiency in engineering, procurement, and service.
The Lenze Smart Motor m300 was developed specifically to meet the requirements of modern conveying systems. It helps machine builders and conveying system manufacturers reduce engineering, procurement, and service costs while standardizing their drive concepts. The solution has proven itself worldwide in conveying applications and is currently in use in more than a quarter of a million installations.
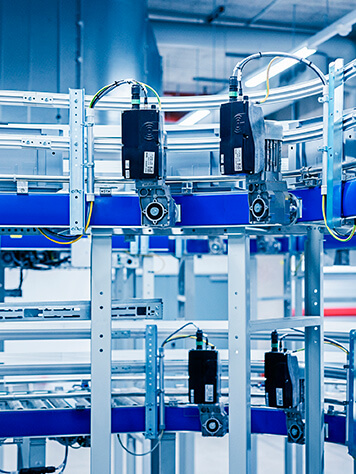
Increasing variant diversity increases the effort required for engineering, procurement, warehousing, and service. The Lenze Smart Motor m300 was developed to reduce precisely this complexity and provide a standardized drive concept for horizontal conveying systems. Its widespread acceptance in the market demonstrates that reducing variant diversity and standardizing drive concepts have become key competitive factors for many conveying system manufacturers.
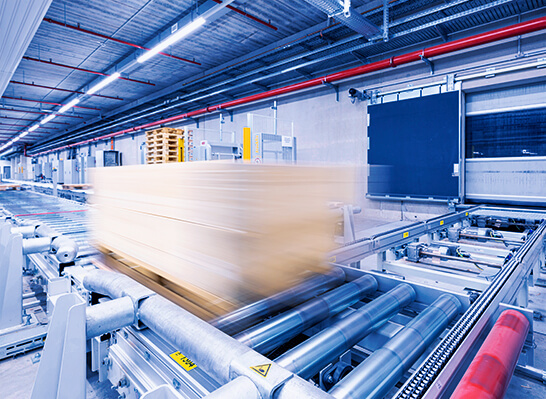
This concept truly shines in applications with frequent start-stop cycles, short cycle times, and a large number of installed drives. The range of applications extends from conventional material handling to conveyor lines for heavy loads of up to 6.8 metric tons—regardless of whether the application operates in standard, fresh, or frozen food environments.
Typical applications include roller conveyors, belt conveyors, chain conveyors, corner transfer unit, and transfer cars in modern conveying and material-handling systems.
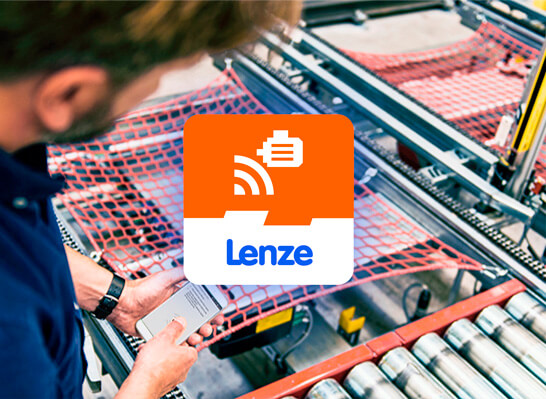
In addition to standardization, ease of use is one of the Smart Motor’s key advantages. Parameterization is performed via NFC directly using a smartphone or PC. The motor does not need to be powered on for this, and no addressing is required. This significantly reduces the effort involved in commissioning and service.
NFC directly via smartphone or PC. The motor does not need to be powered on for this, and no addressing is required. This significantly reduces the effort involved in commissioning and service.
 Less engineering effort
 Fewer variants
 Simplified drive design
 Reduced inventory levels
 Faster commissioning
 Simplified spare parts management
 Higher standardization
 Less complexity throughout the entire lifecycle